The Factory Reality Gap
Why Good Manufacturing Systems Break Down at the Point of Work
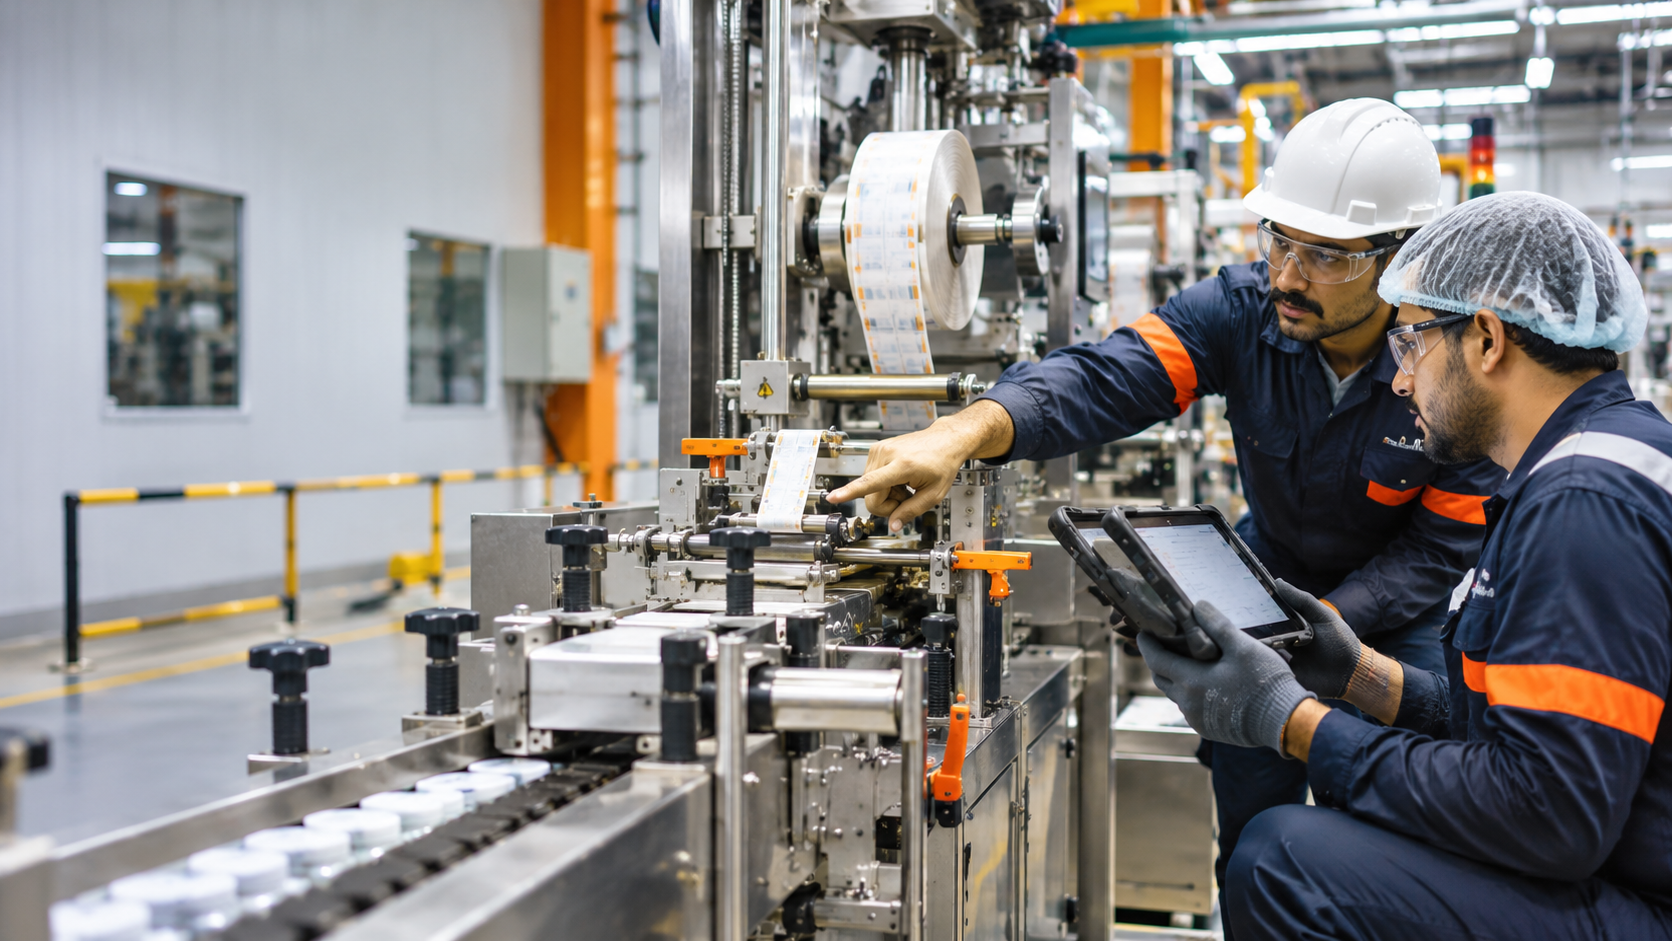
A production line is ready for a changeover. The approved work instruction is available. The operator has been trained. The machine is in working condition.
But the instruction shows the previous product format. A guide position has changed. The label roll is different. The operator pauses and waits for someone familiar with the latest setup to confirm what should happen next.
The procedure exists. The people are present. The equipment is available. Yet the task cannot move forward with confidence.
This illustrative situation captures a familiar manufacturing gap: what the factory has designed is not always what the person encounters when doing the work.
A system can be complete on paper and still be difficult to use in practice.
The issue may be a mismatch between instructions, equipment, information, responsibilities and actual operating conditions. Understanding that mismatch is the starting point for closing the factory reality gap.
1. A System Can Exist Without Supporting the Work
Manufacturing organisations define work through SOPs, training, equipment, safety controls and digital systems. Their presence alone does not tell us whether a task can be performed as intended.
A procedure may be approved but difficult to access at the machine. Training may not prepare a person for a changed condition. A machine may have safeguards, but the work arrangement may make the safe method difficult to follow. A digital record may exist, but the person who needs it may not know where to find it.
There is a difference between having a system and having one that supports work.
This is not about lowering standards or treating procedures as optional. It is about checking whether arrangements are usable under the conditions in which people work.
2. Work as Designed and Work as Performed
Every task has an intended method, defined in an SOP, maintenance instruction, permit, machine setting sheet or sequence of approvals.
That is work as designed.
The task takes place in a real environment. People respond to the equipment, material, time window, machine condition, available information and decisions made by other teams.
That is work as performed.
The two should support one another. When they differ, the difference deserves attention.
The UK Health and Safety Executive recommends designing procedures around the task and user, involving the people who use them and examining how work is carried out. HSE guidance on procedure design.
A procedure should be assessed not only as a document, but as a tool used to complete a task.
3. Where the Reality Gap Forms
The gap rarely comes from one source. It often develops where several conditions meet.
Information gap. The instruction, drawing, asset detail or hazard information exists, but is difficult to locate or interpret at the point of work.
Equipment gap. The machine, tool or layout has changed, while the available instruction still reflects an earlier arrangement.
Timing gap. A shift handover, maintenance update or process change does not reach the next team before a decision is needed.
Responsibility gap. Ownership becomes unclear when work moves between production, maintenance, engineering and safety.
Condition gap. The method assumes stability, but the task involves different material, access, staffing or equipment conditions.
These are prompts for investigation, not assumptions about the cause.
The important question is not simply, "Who did not follow the system?" It is, "What did the person encounter, what did the system expect, and where did the two stop matching?"
4. Workarounds Are Signals Worth Understanding
When a system does not support the task, people often find a way to keep work moving.
They may call an experienced colleague, use a local note, repeat a check, seek clarification or delay the task until the right person is available.
Some adaptations help people deal with normal variation. Others may introduce risk, bypass a required control or create dependence on informal knowledge.
A workaround does not, by itself, prove that a worker is careless or that a procedure is wrong. It tells the organisation that the intended method and the conditions of work may not fit together.
The UK's Health and Safety Executive notes that people adapt to poorly designed jobs, equipment or environments, and that these adaptations can affect health, safety and the wider work system. HSE guidance on human factors.
Understand why a workaround exists before deciding what to change. Removing it without fixing the underlying condition can leave the difficulty in place.
5. Look at the Conditions, Not Only the Person
When a task is delayed or a procedure is not followed, the first explanation can be that someone needs more training or closer supervision.
That may be true, but it should not be the automatic conclusion.
Ask:
- Was the correct instruction available where the task took place?
- Did it match the current machine and operating condition?
- Could the person understand what was expected?
- Were the required tools, time and access available?
- Were responsibilities clear?
- Was there a defined response for an unexpected condition?
A training record confirms that training was completed. It does not demonstrate, by itself, that the instruction was understood and usable in the actual task.
OSHA guidance emphasises that training should use language and vocabulary workers can understand and relate to practical workplace needs. This is general guidance, not a substitute for applicable Indian requirements or site-specific obligations. OSHA training guidance.
A person should not have to compensate indefinitely for a system that is difficult to understand or use.
6. The Point-of-Work Reality Test
Follow one task from preparation to completion and ask:
- Can the person identify the task and equipment? The correct asset, location and operating condition should be clear.
- Can the person access the required information? Instructions, drawings, hazards and controls should be available when needed.
- Does the information match the current condition? Changes to equipment, material, method or layout should be reflected in the guidance.
- Are responsibilities clear? People should know who decides, who performs the work and when escalation is required.
- Can the person respond when the sequence changes? The system should make it clear when to stop or seek guidance.
- Can completion be checked? The organisation should confirm that the task was completed and relevant controls restored.
The purpose is to reveal where the intended method loses support in the real workplace, not to create another checklist for its own sake.
7. The Gap Is Shared Across People, Machines and Processes
The factory reality gap is rarely only a people issue, a machine issue or a procedure issue.
People bring skills, experience, judgement and the ability to recognise unusual conditions. They also work within limits of attention, time and information.
Machines have physical states, access points, controls, limitations and maintenance requirements. A change to equipment can affect how a task should be performed.
Processes define the expected sequence, controls, approvals and handovers. They need to reflect the actual work.
Information connects these elements. It helps people identify the machine, understand which method applies, recognise changes and know what must happen next.
If one element changes without the others being reviewed, the gap can widen. A machine modification may require updated instructions. A revised procedure may require communication and training. A digital workflow may need to reflect who actually approves and performs the task.
The aim is to keep these elements compatible as the workplace changes.
8. Where BRIGS Can Help
Closing the factory reality gap requires understanding the conditions around the work before selecting a solution.
Factory U/X addresses how people interact with the workplace. Visual information, equipment identification, signage, markings and navigation can make the intended action easier to recognise.
Factory O/S supports the movement of information and operational workflows. Digital SOPs, maintenance activities, permits and audits can help make relevant information available to the people who need it.
M/P Safety addresses machine and process risks through assessment and appropriate controls, including guarding, interlocking, LOTO and process safety measures.
These are different intervention areas, not interchangeable fixes. An identification issue may need a visual solution, a fragmented workflow a digital one, and a hazardous access point an engineered safeguard. Some conditions need a combination.
The right response depends on what the investigation finds.
9. Diagnose Before Deciding What to Change
The BRIGS approach follows six connected stages:
SEE the task as it is actually performed. Observe where people stop, search, wait or adapt the method.
CONNECT the conditions around it. Examine the people, equipment, information, responsibilities and controls involved.
DIAGNOSE the point of mismatch. Establish whether the gap relates to usability, equipment, information, workflow, safety or a combination.
DESIGN an intervention that addresses the identified condition.
IMPLEMENT the change in the operating environment, with the people who will use it.
IMPROVE by checking whether the task has become clearer, safer and more reliable—and whether a new difficulty has appeared elsewhere.
This sequence avoids assuming that every problem needs software, training, another procedure or more supervision.
10. Make the System Work Where the Work Happens
A manufacturing system should be judged by more than the documents it contains, the equipment it has installed or the software it uses.
It should also be judged by how well it supports the people expected to use it.
Can they understand what is required? Can they identify the right equipment? Can they access current information? Can they act within the necessary controls? Can they deal with changing conditions without relying entirely on informal help?
The objective is not to remove every variation. The system should recognise changing conditions and give people the information, controls and responsibilities needed to respond.
The factory reality gap is the distance between what the system expects and what the workplace makes possible.
At BRIGS, understanding that distance is the starting point for designing practical improvements across visual workplace systems, digital operations, machine safety and process safety.
A system is not effective simply because it has been documented, installed or approved.
It becomes effective when it supports the work where the work actually happens.
More from Brigs
Understanding the Factory as a Process
Understand how people, machines, processes and information work together—and why gaps between them can disrupt everyday factory operations. Explore how BRIGS identifies these gaps and improves the workplace through Factory UX, Factory OS, safety and process improvement.
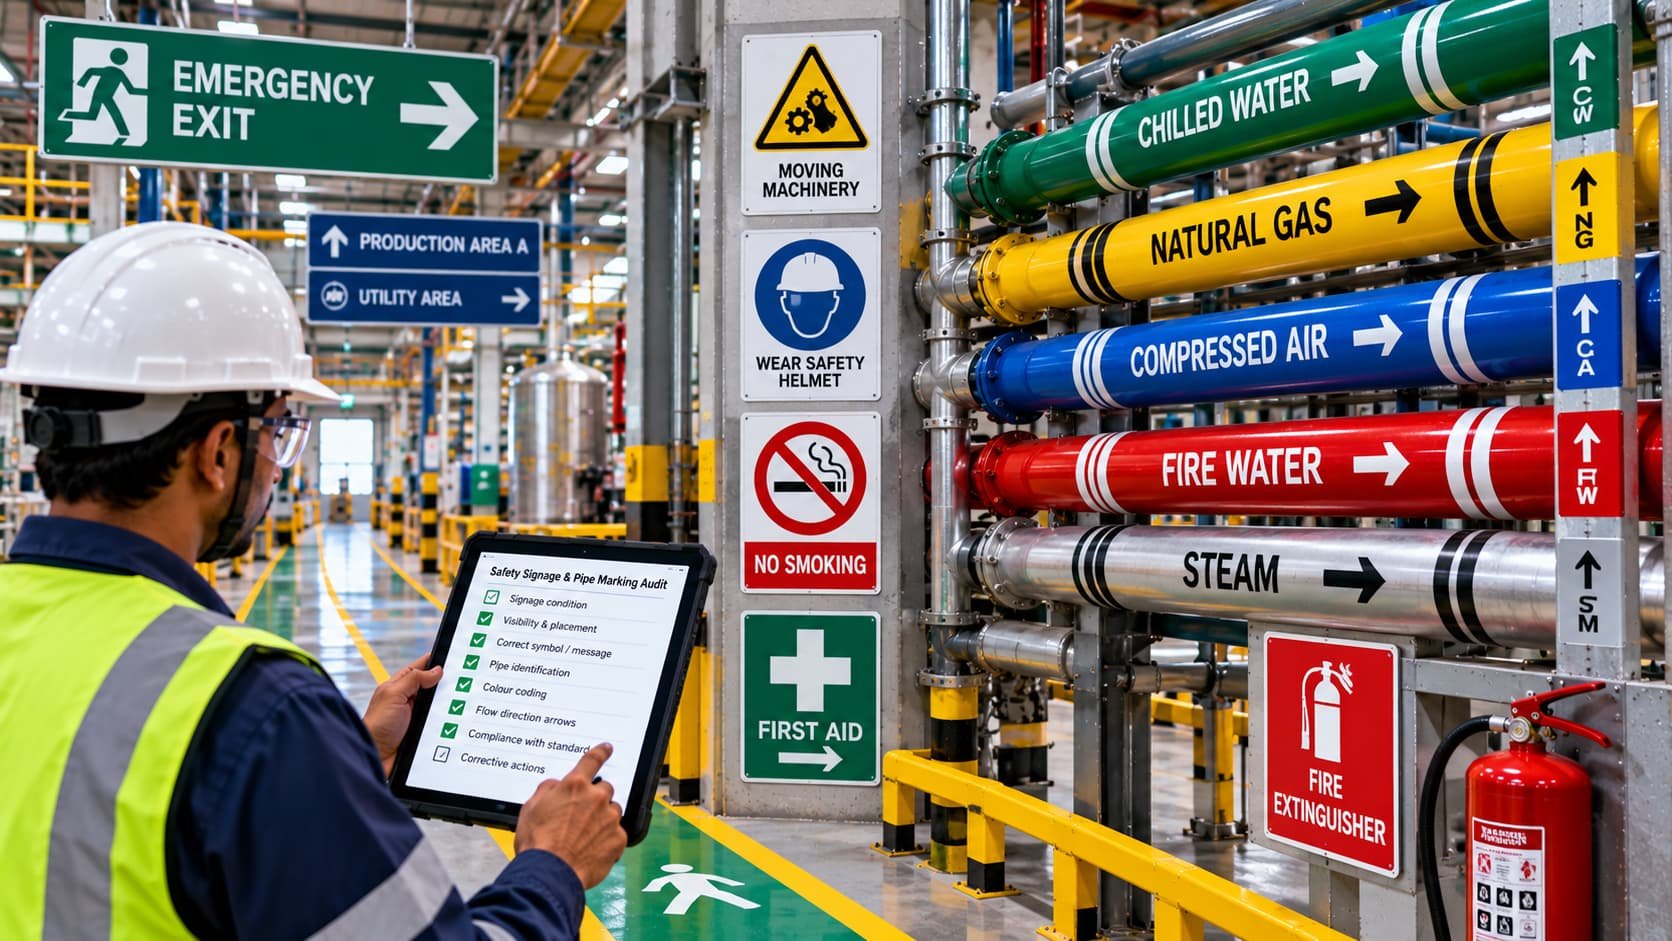
Safety Signage and Pipe Marking: When the Factory Itself Communicates Safety
A warning sign should not need an explanation. A pipeline should not need to be traced to understand what it carries. In a well-designed industrial workplace, critical information is visible before someone makes a decision.
Digital Transformation in Manufacturing: Why the Last Mile Matters More Than Another Dashboard
Factories have dashboards, analytics and real-time reports. But does the worker at the machine have the right information at the right time? Why digital transformation must reach the last mile.
Have a similar challenge on your site?
Tell us what you are trying to improve and we will help you find the practical next step.